Household Air Purifier Factory Quality Control Steps Every Importer Should Verify
2026-09-28
Most importers only realize their air purifier supplier skipped critical quality checks when customers start complaining of burning smells or failing motors. By then, the damage is done. The truth is, you can verify every essential factory control step before your order ships—if you know what to look for. At LUFUTATECH, we walk you through the exact checks that separate a dependable production line from a warranty nightmare.
Raw Material Gatekeeping: What to Inspect Before Assembly Starts
Before any wrench turns or solder flows, the incoming material bench is where a lot of future failures get caught—or missed. Start with the paperwork, but don't stop there. Match the mill cert or certificate of conformance against the actual heat lot or batch number stamped on the stock. If those don't line up, stop the line before it starts. Then pull a physical sample from each pallet, not just the top sheet or the easiest box to reach. A quick caliper check on thickness, width, and hole diameters can reveal a supplier drift that a glossy C of C won't mention.
Beyond dimensions, think about what the material will go through later. For metals, hardness and temper are the usual suspects—soft 6061 can turn a simple bracket into a warranty claim after a few thousand cycles. For composites, laminates, or wood, moisture content matters more than almost anything else because it changes fit after assembly. A handheld durometer or moisture meter costs little and takes seconds, but it can keep a bad batch from becoming next month's field failure. Also check surface conditions: deep scratches, edge dings, or oxidation that will telegraph through plating, painting, or anodizing.
Finally, organize what you reject as carefully as what you accept. Tag quarantined stock with the reason, lot number, and date, and park it somewhere it can't accidentally find its way back into the production flow. Circle back with the supplier using photos and measurements, not vague complaints. Raw material gatekeeping is less about being difficult and more about buying yourself a clean start. If the stock isn't right before the first operation, no amount of careful assembly downstream will fix it.
The Line Checkpoints Most Factories Skip (But You Shouldn't)
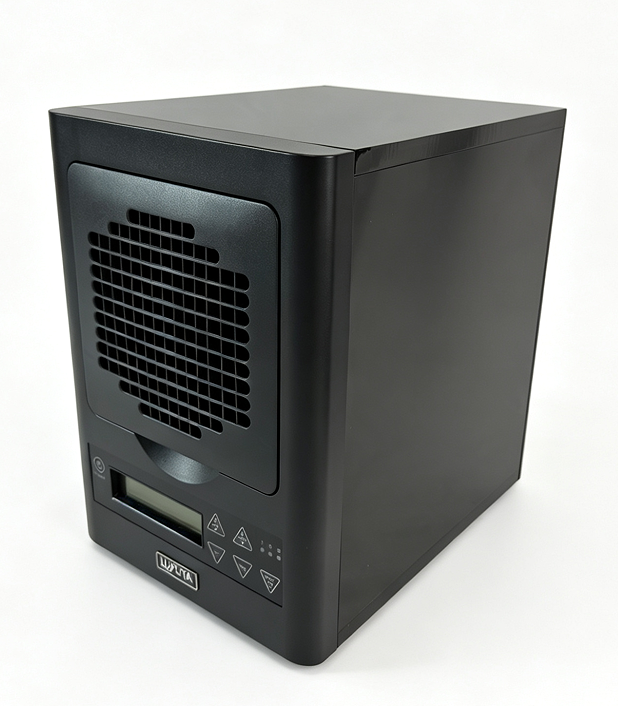
It is easy to walk past a checkpoint that seems redundant when the line is running smoothly. The first-off inspection after a material lot change, the torque check after a seating operation, the quick scan for debris before a gasket goes down—these are the ones that get waved through because the last shift did them or because the customer is waiting. But these small pauses exist for a reason. They catch the drift that happens between operators, the wear on a fixture, or the batch of slightly undersized fasteners that looks fine until it is under load.
Skipping them does not save time; it moves the cost downstream. A label printed with yesterday's date code might not matter at the end of the line, but it becomes a recall risk after shipping. A skipped torque verification on a single bolt can turn into a field failure that costs more than a month of line stops. The checkpoints worth keeping are rarely dramatic—they are the ones that feel repetitive, which is exactly why they work. If a factory does not have a written reason for skipping a checkpoint, it should not be skipped.
End-of-Line Performance Runs That Expose Weak Motors
Every motor leaving the floor gets a short but demanding sequence of full-load starts, rapid reversals, and a sustained high-torque hold. This isn’t a pass/fail formality. The runs are tuned to catch the units that look fine on a winding resistance check but fall apart once real current flows through them. A weak rotor bar, uneven air gap, or slightly mis-seated brush often shows up as an unexpected current spike or a drop in rpm under load.
The best lines compare each run against a golden reference trace gathered from a known-good motor of the same batch. Deviations in acceleration time, steady-state draw, or vibration signature trigger a deeper teardown. Over time, these traces become a fingerprint of manufacturing health. When a specific defect keeps appearing, it points back to a forming issue or bearing press variation instead of blaming the motor itself.
Teams that skip this step usually pay for it in warranty claims and line returns. A motor can pass all static tests and still stumble the first time it faces a real coupling. End-of-line performance runs are the only chance to catch that before the customer does. They don’t just verify output; they reveal how the motor behaves under stress, and that’s where hidden weaknesses live.
Certification Paperwork: Separating Real Compliance from Copies
Anyone can run a certificate through a photocopier, but paperwork that actually satisfies a regulator requires more than a matching letterhead. The difference often hides in the small details: wet-ink signatures versus scanned ones, sequential document control numbers, revision dates that align with internal audit trails, and watermark placement that only shows under specific lighting. A genuine compliance file tends to be living — it gets updated when standards change, referenced during training, and pulled out during surprise inspections without hesitation. Copies, by contrast, are usually static and suspiciously clean.
One practical way to separate the two is to ask for the chain of custody behind each certificate. Where did the original training record live? Who signed off on the competency assessment, and can that person be reached for a quick phone call? If a supplier or contractor hands you a binder full of identical-looking documents with no variance in formatting, no human errors, and no evidence of progressive updates, treat it as a red flag. Real compliance paperwork is rarely pristine; it carries coffee stains, marginal notes, and the occasional correction that was properly initialed.
Another angle is to cross-reference the certificate against the actual operational environment. A forklift operator’s license might look valid on paper, but does the equipment on your floor match the type listed? A fire safety certificate for a building wing that no longer exists tells you the document was copied from an old template. When you start checking dates, equipment serial numbers, and instructor names against real-world records, the difference becomes obvious: authentic compliance is verifiable beyond the page, while copies fall apart the moment you ask a second question.
Packaging Abuse Tests That Save You from Freight Headaches
Most freight damage isn't caused by one dramatic drop. It builds up through constant vibration, uneven stacking pressure, and careless handling at transfer points. Running a short battery of abuse tests before your product ships gives you a clear map of where the package will crack, tear, or crush under real conditions.
Start with a drop test using the actual boxed weight and dimensions, hitting the corners and edges that catch the worst impacts. Then place the package on a vibration table to mimic hours of highway and rail movement. Finish with a compression test that simulates a tall pallet load sitting in a warehouse. These three steps reveal nearly every weak point that would otherwise turn into a freight claim.
If your shipment crosses multiple carriers or export hubs, add an incline impact test and a loose-load simulation. An extra hour in the lab now prevents weeks of back-and-forth with carriers, repackaging costs, and product arriving in pieces at your customer's dock.
Unannounced Batch Pulls: The Only Way to Trust Long-Term Quality
Most quality programs rely on scheduled inspections, but those tell you almost nothing about the batches that ship between visits. A supplier can clean up for a day, arrange tidy paperwork, and pass with flying colors while the rest of the year stays messy. Unannounced batch pulls flip that dynamic. When a shipment gets pulled for testing without prior warning, you're seeing the product exactly as your customer would receive it—not a rehearsed version.
The real value shows up over months, not weeks. A factory that never knows when the next lot will be held for lab analysis starts treating every production run as if it's under review. That subtle shift in mindset is what separates genuine long-term consistency from short-term compliance theater. You stop auditing a moment in time and start auditing a pattern of behavior. And pattern is the only thing worth trusting when you're building a brand that has to last.
FAQ
Rather than accepting a generic 'IQC done' statement, ask to see the supplier's sampling plan and rejection log for the most recent three lots. For HEPA or activated carbon filters, confirm they test pressure drop and filtration efficiency against a reference standard, not just visual appearance. Motors should have locked-rotor and winding resistance checks, while plastic housings need melt flow index and flammability rating verification. A missing rejection record or blurry pass/fail criteria is a red flag that cheap substitutions could slip through.
Walk the line and look for in-process checkpoints. At a minimum, there should be torque checks on motor mounts, a jig or fixture to verify fan blade clearance, and a go/no-go gauge for filter seating. Ask operators what they do if a unit fails at their station. If they point to a repair bench and a rework log, that's a good sign. If they simply push the unit forward to be caught at the end, the final inspection becomes a bottleneck and defects get hidden.
Focus on clean air delivery rate (CADR), noise level at highest speed, and power consumption. The spec sheet from the factory is not enough; confirm the test chamber is calibrated and that they use a reference dust or cigarette smoke source. Accept/reject limits should be set from a pilot run, not from the marketing brochure. For example, if the promised CADR is 300 m³/h, allow a tolerance of -5% but reject anything with a noise reading above the declared dB(A) by more than 2 dB. Power consumption should never exceed the label rating by more than 10%.
Ground continuity and leakage current tests on every unit are non-negotiable, but many importers only see a sampling report. Ask whether the factory performs a 100% hipot test on the power cord and PCB assembly before final assembly, not just on finished goods. Also verify that internal wiring near the fan has abrasion protection and that the ionizer, if present, has a current-limiting circuit. A unit that passes a one-time bench test can still short out after vibration during shipping if wire routing is not checked on the line.
Request the incoming inspection correlation data between filter lot and motor lot. A well-run factory will have a matrix showing which filter batch was paired with which motor batch during assembly, along with any adjustments made to fan speed or sealing gaskets. If they treat every filter as interchangeable without verifying fit, you risk air bypass that destroys CADR. Ask to see an actual filter fit test on a random assembled unit: hold a smoke pen near the filter seal to check for leaks.
A short burn-in catches infant mortality failures like bad solder joints or a fan that seizes after thermal expansion. For household air purifiers, a 30-minute run at maximum speed with an ambient temperature of 40°C is usually enough to reveal early defects. If the factory only runs the unit for five minutes to check that the LED lights up, that's not a burn-in; it's a power-on test. Ask whether they record any units that fail during burn-in and what corrective action is taken.
Check that the carton drop test has been performed on a sample from the same production lot, not just a pre-production prototype. Look at the labeling on the unit and the power cord: the safety marks should match the country of destination, and the rated voltage should not have a sticker placed over a different printed value. Also verify that the user manual's filter replacement instructions match the actual filter model packed inside. Mismatched manuals or vague voltage labels often indicate last-minute changes without proper re-validation.
Ask for the original handwritten or electronic test logs for a specific serial number range, then trace two or three units backward to their production date and test station. Check if the timestamps and operator signatures align with shift schedules. Inconsistent handwriting, identical test values across many units, or missing entries for a day when the factory claims full production are signs of data padding. A better approach is to have your own inspector randomly pull units from the line and witness the same tests being performed, comparing results to the factory log.
Conclusion
Most importers only find out about weak solder joints or undersized HEPA seals once returns start piling up. That is why the first walkthrough has to happen at raw material intake: check the melt flow index on ABS batches, verify fan motor winding resistance against the approved sample, and reject any filter media rolls without lot-level efficiency data. On the line, do not settle for the standard final once-over—insist on spot checks after ultrasonic welding and around the carbon filter cavity, because that is where dust bypass usually creeps in. Then watch a unit run full speed for at least 30 minutes straight; a motor that grows noisy or a CADR reading that dips below claim after warm-up tells you more than any certificate.
Paperwork alone is not enough. Compare the safety mark layout against the lab's public database, and call the certifier if the factory's test report shows a different plug type than what is actually in the carton. Packaging matters just as much: run a corner drop from 76 cm with the unit inside its retail box and inspect the internal foam compression afterward—crushed corners are a freight damage claim waiting to happen. Finally, schedule unannounced pulls every two or three production days. Grab a sealed carton at random, tear it down in front of the line supervisor, and run it through the same in-house tests your lab uses. Consistency in those surprise batches, not in a handpicked golden sample, is what separates a factory you can reorder from one you will be chasing with chargebacks.
Contact Us
Contact Person: Paul Luo
Email: [email protected]
Tel/WhatsApp: 0086-19966314501
Website: https://www.lufutatech.com