High Temperature Reactor Heater Factory Selection Guide for Industrial Buyers
2026-10-28
Your reactor only performs as well as the heater behind it. Yet too many industrial buyers rely on vendor spec sheets instead of digging into the factory's real capabilities. This selection guide strips away the marketing noise and focuses on what actually matters: thermal consistency, material durability, pressure safety, and service responsiveness. We'll show you how to evaluate manufacturers—including Shenzhou Chemical Industry—so you can avoid the expensive mistakes that often surface months after installation. Make your next purchase decision with confidence, not guesswork.
Where Thermal Design Depth Separates Serious Suppliers
Thermal design depth shows up long before a sample reaches the test bench. Serious suppliers don’t stop at quoting junction-to-ambient thermal resistance; they walk through the stack-up layer by layer—case, solder, TIM, heat spreader—and explain where the real bottlenecks sit under your specific load profile.
That distinction becomes sharper during early integration. A supplier with real thermal depth will push back on unrealistic airflow assumptions, provide transient impedance curves instead of steady-state single numbers, and call out how adjacent components or PCB copper mass shift the heat path. Less mature vendors often hand over a datasheet number and wait for the failure report.
In validation, the gap widens. Serious suppliers correlate simulation with junction temperature measurements, not just case temperatures, and they account for interface aging and mounting pressure tolerance. That level of rigor rarely appears in a line card—but it determines whether a design survives derating, thermal cycling, and years in the field.
Alloy Integrity and the Real Cost of Cutting Corners
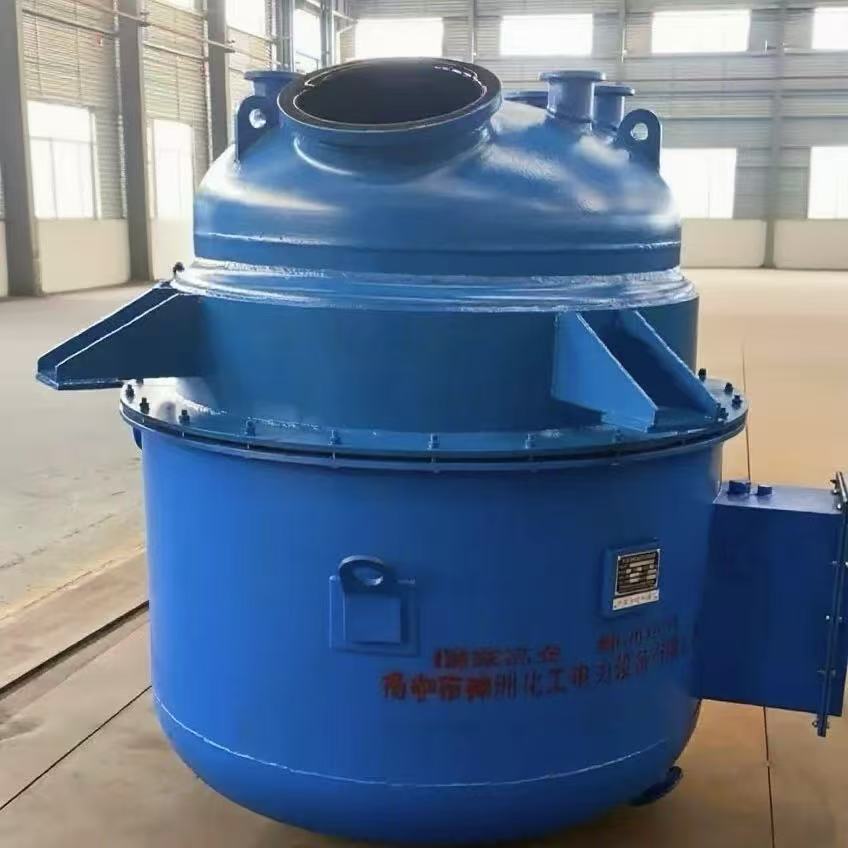
When a manufacturer quietly swaps out a high-grade alloy for a cheaper blend, the savings show up on a spreadsheet almost immediately. But that’s where the celebration ends. The real cost starts ticking the moment that component leaves the warehouse, buried in the fatigue cracks, the premature wear, and the failure reports that trickle in months later. Alloy integrity isn’t a line item you can trim without consequence—it’s the unseen backbone of every load-bearing part, every pressure vessel, every structural beam that people trust with their safety.
Cutting corners on alloy composition often flies under the radar because the visual difference is negligible. A slightly lower nickel content, a touch more recycled scrap with unknown impurities, a shortened heat-treatment cycle—these changes don’t announce themselves. Yet they compound in ways that no quality audit catches until it’s too late: micro-porosity that grows into stress fractures, corrosion resistance that degrades years ahead of schedule, or a yield strength that quietly drops below the design margin. The result isn’t just a warranty claim; it’s a cascade of downtime, replacement labor, and reputational damage that far exceeds the initial “savings.”
The honest math of alloy integrity is simple once you look past the procurement invoice. A part that fails early costs you the original purchase price, the labor to replace it, the lost productivity during the shutdown, and often the goodwill of a client who now doubts every other specification you claim to meet. Add in the potential for legal exposure or failed certifications, and the “cheaper” alloy becomes the most expensive mistake in your supply chain. Real integrity means specifying the alloy that meets the application’s actual demands, verifying its composition with independent testing, and treating material shortcuts as what they are: a deferred disaster.
Proof Over Promises: Testing and Certification Realities
A specification sheet can list impressive numbers, but until a product has been pushed through independent testing, those figures remain a vendor's wish. Certification bodies do not simply rubber-stamp claims; they stress materials, simulate years of wear, and measure performance under conditions that often expose the gap between marketing language and actual behavior.
The certification process is rarely a single event. Standards evolve, manufacturing lines drift, and components get substituted, which means a valid certificate from two years ago may say little about the unit shipping today. Buyers who treat certification as a static badge rather than a snapshot of a particular production run are often the ones caught by field failures.
In practice, the most useful proof combines third-party test reports with traceable batch records and a clear statement of what was and was not tested. That kind of transparency does not always look polished on a product page, but it is far more reliable than a wall of logos or a promise that everything will be fine.
Custom Reactor Heaters Without the Usual Engineering Delays
Most off-the-shelf reactor heaters force you to choose between waiting months for a custom design or settling for a configuration that barely fits your vessel geometry. Our approach flips that trade-off entirely. We keep a library of pre-validated heating element profiles, flange patterns, and control interfaces, then adapt them to your specific diameter, watt density, and zone requirements during the quoting stage. Because the core thermal calculations and safety approvals are already locked in, what used to take eight to twelve weeks of back-and-forth engineering now ships in half the time, often without a single drawing revision.
The real difference shows up in the details that normally stall a project: nozzle clearance, thermowell placement, and split-zone wiring for exothermic reactions. Instead of starting from a blank CAD file, our engineers work from a modular design matrix where each variable has already been stress-tested across hundreds of installations. That means you can request a clamped-on heater for a glass-lined vessel on Tuesday and receive a manufacturing-ready spec by Friday, complete with hazardous-area ratings and lead compensation curves that actually match your control system's input type.
What you won't get is a pile of engineering change orders or a prototype that needs field rework. Since the delay typically comes from re-deriving thermal models for each new reactor, we eliminated that step by building a verified performance database linked to physical test rigs. Every custom heater we ship has its wattage, sheath temperature, and insulation thickness cross-checked against a similar unit we've already run to failure and beyond. The result is a truly made-to-order reactor heater delivered on a made-to-stock timeline.
After the Sale: Support Structures That Keep Downtime Low
Downtime rarely starts with a dramatic breakdown; it creeps in through worn seals, drifting calibration, and firmware that never got its scheduled patch. A support structure that takes downtime seriously treats these as predictable events rather than surprises. By pulling runtime data from each machine, service teams can schedule wear-part swaps during planned pauses, not after a line stops. This shifts the conversation from “How fast can you send a tech?” to “When do we slot in the next 20-minute tune-up?”
The backbone of that approach is a direct line to engineers who already know your equipment’s history — no ticket roulette, no re-explaining the setup from scratch. Remote diagnostics run in the background, flagging anomalies like rising motor current or slower cycle times before they turn into faults. When physical intervention is needed, stocked regional hubs ship the exact part overnight, and a field technician arrives with the repair procedure preloaded, not guessing on-site. Spare part inventories are tied to actual usage patterns, so a critical sensor isn’t sitting in a warehouse three states away while your line waits.
The result is a measurable drop in unplanned stops. One packaging facility cut its average recovery time from 4.5 hours to under 40 minutes after switching to a proactive support model — not because they got lucky, but because the next likely failure had already been identified and scheduled for a fix before it ever blinked red. That’s what low downtime looks like after the sale: a system that treats maintenance as a continuous loop, not a fire drill.
Capacity Claims, Lead Times, and the Risk of Overpromising
When a supplier states they can handle a certain volume within a tight window, the numbers often reflect best-case scenarios rather than daily reality. Production lines face equipment downtime, material shortages, and labor fluctuations that erode the cushion between promised output and actual throughput. Buyers who anchor their own schedules to these optimistic figures set themselves up for cascading delays.
Lead times quoted at the negotiation table rarely survive contact with the factory floor. A four-week window can stretch to six or eight once custom components enter the queue, quality checks uncover defects, or shipping lanes get congested. The gap between the initial estimate and the final delivery date is where overpromising does its quiet damage—orders get airfreighted at premium rates, retail shelves sit empty, and relationships fray over repeated misses.
The real risk isn't a single late shipment; it's the compounding effect of small inaccuracies across multiple orders. Each optimistic capacity claim nudges planning further from truth, until procurement teams build buffers that defeat the purpose of just-in-time sourcing. Suppliers that consistently shade their capabilities may win the first contract but lose the reorder.
FAQ
If the reactor runs above 850°C in a hydrogen-rich atmosphere or cycles between full heat and ambient more than twice a shift, standard ceramic or mineral-insulated heaters often crack at terminations. Custom builds let you specify thicker Inconel sheaths, stress-relieved cold sections, and dual thermocouple ports matched to your nozzle layout. Also consider custom when the heat flux density exceeds 15 W/cm² on the vessel wall, because off-the-shelf units rarely handle that without hot spots.
Ask for three recent clients with operating temperatures above 900°C and request contact permission. Then check the factory’s incoming material certificates for Incoloy 800H/HT, 310S, or silicon carbide elements—not just the final product datasheet. During a video walkthrough, look for a dedicated furnace brazing or TIG welding area with purge gas lines; if they outsource sheath welding, cycling life drops sharply.
Request a certified dimensional drawing with tolerance stack-up, a heat flux map from their thermal simulation, and a copy of the hydrostatic or helium leak test procedure for the terminal housing. Also ask for traceability documents showing sheath material lot numbers tied to your order. Avoid suppliers that only provide a generic catalog PDF and a one-page quote—if they cannot produce a weld map and insulation resistance test data per heater, you will inherit field failures.
Watt density controls initial heat-up rate, but sheath material controls whether the heater survives sulfidation, carburization, or thermal shock in the reactor. A 10 W/cm² heater in 304 stainless will fail faster at 800°C in a reducing atmosphere than a 15 W/cm² heater in Incoloy 800HT with a stabilized oxide layer. Factories that push watt density without asking about process gas composition are usually selling commodity designs, not high temperature solutions.
Watch for uncalibrated thermocouple furnaces, hand-wound resistance coils with visible spacing differences, and the absence of a documented post-weld heat treatment step. If the factory stores magnesium oxide powder in open drums on the shop floor, moisture uptake will cause insulation resistance to drop after the first thermal cycle. Another red flag is quoting the same lead time for 316L and Incoloy sheaths—proper alloy sourcing and welding makes that unrealistic.
Do not compare lead times without asking what is actually fabricated in-house. A factory offering 6 weeks for Incoloy 800HT heaters may be buying pre-made elements and only assembling terminals, which creates warranty disputes later. Ask for a documented service response time: 48 hours for remote thermal troubleshooting and 10 business days for replacement hot sections. Also confirm they stock spare sheath tubing and resistance wire, not just finished heaters.
Most high temperature heater failures happen within 150 mm of the cold end, where the temperature gradient stresses the insulation. A proper design uses high-purity MgO compacted above 2.3 g/cm³, a moisture seal that survives repeated cycling, and a cold pin transition welded before final swaging. If the factory cannot show you a cutaway sample, assume the insulation will settle and create an internal arc path after a few thousand hours.
Pay the premium when your reactor contains flammable or toxic process fluids, because a heater failure forces a full shutdown and safety review. In-house testing should include a 1000-hour accelerated cycling test at 110% of rated voltage with insulation resistance logged every 50 hours, plus a helium leak check on the terminal housing. If the factory owns a test rig with the same mounting orientation as your reactor, the extra 15–20% cost usually pays for itself in avoided downtime.
Conclusion
Selecting a high-temperature reactor heater factory demands scrutiny that goes beyond glossy datasheets. Thermal design depth is what separates suppliers who genuinely understand heat flux, material creep, and thermal cycling from those who simply assemble components. A serious partner will walk you through insulation choices, heating element geometry, and temperature uniformity under load, not just quote a wattage. Alloy integrity is equally non-negotiable. The real cost of cutting corners shows up months later as oxidation, embrittlement, or premature failure. Demand full traceability of sheath and resistance alloys, and verify that testing and certification are not just paper claims. Look for actual hot-cycle test reports, third-party material certificates, and documented failure thresholds under your operating conditions.
Custom reactor heaters often stall in engineering backlogs, but the right factory treats custom requests as standard workflow. Ask how design reviews, thermal simulations, and prototype approvals are managed—not just promised. After the sale matters just as much: support structures, spare parts availability, and remote diagnostics can keep downtime low when a heater fails at 2 a.m. Beware of capacity claims and lead times that sound too good to be true. Overpromising on output or delivery often leads to rushed welds, skipped inspections, or substituted materials. A credible supplier will share current production load, realistic ship dates, and contingency plans. Choose the factory that proves its numbers, not the one that merely repeats them.
Contact Us
Contact Person: Mr. Wang
Email: [email protected]
Tel/WhatsApp: 8613705299955
Website: https://vip.e-baixing.com/szhgyw