Gobo Projector Factory: Inside the Craft of Custom Light Pattern Production
2026-10-22
Before a custom light pattern ever hits a dance floor or gallery wall, it starts as an idea inside a gobo projector factory. There, precision optics meet hands-on craft—and TNT has spent years turning that intersection into reliable, one-of-a-kind projections.
Where Custom Light Patterns Start
Every custom light pattern begins with a single question: what do you want the space to feel like? It might be a quiet corner that needs a soft, rolling glow, or a storefront that calls for crisp, attention-grabbing movement. The answer rarely comes from a catalog, because the most memorable lighting starts with observation, not selection.
From there, the process moves into mapping. We look at the surfaces, the angles, the moments people actually spend in a room, and start sketching out rhythm, intensity, and color. A pattern is not just a sequence of lights turning on and off; it is a conversation between the fixture and the architecture. That conversation is where customization truly begins.
Only after the intent and the space are understood do we start layering in technical details, such as timing curves, fade lengths, and brightness constraints. This keeps the work grounded, so the final result feels less like a preset effect and more like something the room was always meant to do.
Cutting Steel Without Losing the Art
There is a quiet violence to the first cut. A blade meets steel, and the room fills with a high, metallic whine that sharpens into a scream. Sparks scatter like startled fireflies, tracing brief, bright arcs before dying on the floor. Yet for the hands guiding the tool, this is not destruction. It is a conversation. The steel resists, then yields, and in that yielding, a shape begins to emerge. The trick is not to overpower the material, but to listen to it.
Most people assume that cutting steel is purely mechanical—a matter of force and precision. But ask any seasoned fabricator, and they will tell you the real skill lies in restraint. You do not rush a cut. You let the blade find its own rhythm, adjusting pressure by feel rather than by eye. The line you are chasing is already inside the metal; your job is to reveal it without erasing the small imperfections that give the work its soul. A perfectly straight edge is easy. A cut that retains the memory of being cut is rare.
The modern world has given us lasers, water jets, and computer-driven torches. They are remarkable for speed and repeatability. But they also remove the hands from the process, and with the hands, something goes missing: the slight waver, the almost invisible deviation, the breath held for just a second too long. True craftsmanship in steelwork is not about eliminating those marks. It is about deciding which ones to keep. When you cut steel without losing the art, you are not just shaping metal. You are preserving the conversation between maker and material, one spark at a time.
Why Off-the-Shelf Gobos Fall Short
Off-the-shelf gobos are built for the average fixture, not yours. Their image size, focal length, and steel thickness are compromises that leave you with soft edges, uneven hotspots, or patterns that feel lost in the room. A design that looks sharp in a 19-degree barrel can turn muddy when you drop it into a 36-degree unit, and stock options rarely give you the exact specs needed for a clean projection.
Then there's the heat. Most stock gobos are stamped from thin stainless steel, which starts to warp after a few hours in a high-output LED or tungsten fixture. As the metal bends, fine details blur and can eventually burn through. Custom gobos, by contrast, are available in thicker steel, aluminum, or even glass, so they hold their shape and keep the pattern readable through long runs.
The biggest letdown, though, is the library itself. You're stuck choosing from a handful of generic shapes and tired breakup patterns that have no connection to your show, brand, or space. A stock gobo can't give you a specific logo, a particular leaf silhouette, or a texture that follows the geometry of your set. It will always feel like a placeholder rather than an intentional part of the design.
The Quiet Precision of a Gobo Factory Floor
The floor doesn't roar; it murmurs. Rows of laser cutters hum behind tempered glass, their beams tracing hairline patterns into sheets of stainless steel and borosilicate. Each machine moves with a patience you almost never see in a production space—no clatter, no rush, just the soft exhale of air knives clearing away microscopic debris.
Workers at inspection stations lean into task lamps, holding finished gobos at an angle so the etched edges catch the light. What looks like a simple circle or shutter cutout reveals, under magnification, a landscape of tiny facets and deliberate imperfections meant to shape a beam hundreds of feet away. There is no chatter here; a nod or a raised eyebrow passes between shifts, but the room stays tuned to the frequency of careful hands.
Even the packaging area keeps the same rhythm. Each gobo settles into its foam-lined envelope with a faint click, as if the floor itself knows that one wrong move could blur a stage picture or soften a hard edge. Quietness, here, is not emptiness. It is the sound of precision taking its time.
From Digital File to Physical Beam
A CAD model of a steel beam rarely survives contact with the shop floor unchanged. The neutral file—often a STEP or DXF exported from Tekla or SolidWorks—gets broken into discrete toolpaths, kerf allowances, and hole locations. What started as a clean 3D extrusion becomes a set of instructions that a CNC drill line or plasma cutter can follow without human interpretation.
On the fabrication line, that digital data meets the physical constraints of raw material: mill tolerance, residual stress, and heat distortion. The operator may nudge a cut sequence or reorder hole drilling because a flange is 2 mm thicker than nominal. These small corrections are not failures of the model; they are where the digital double gets forced into reality.
The finished beam still carries its digital origin. Part numbers etched by laser, bolt patterns within a millimeter of the model, and weld maps linked to the original file all trace back to the same source. The digital file does not simply describe the beam—it prescribes the steps that make it. And yet, the beam only becomes trustworthy when someone has read the drawing, checked the steel, and watched the first arc strike.
What Happens When a Pattern Meets Its Lamp
Most people think a pattern lives on paper, tile, or fabric—static, obedient, predictable. But place it in front of a lamp and the whole story changes. The light strips away its flatness, bending every curve and stretching every gap until the pattern starts speaking in shadows. What was once a neat little grid becomes a tangle of dark veins on the wall, breathing with each flicker of the bulb. The lamp doesn't just illuminate; it interrogates. It asks the pattern: how do you hold up when I push you through glass, through shade, through the dust in the air?
And then the real meeting happens—not on the surface where the pattern was born, but in the space around it. A floral motif turns into a ghost garden. A geometric border throws itself across the ceiling like a broken ladder. The lamp becomes a translator, turning repetition into rhythm, symmetry into surprise. Sometimes the pattern fights back, refusing to be reduced to a mere shadow; it catches the light at an angle and shatters it into a thousand tiny refractions. In that moment, neither pattern nor lamp is the same. They've made something new—a temporary, glowing argument that disappears the instant you hit the switch.
FAQ
A gobo projector is essentially a lighting fixture that throws a shaped beam of light, using a stencil-like disc inside to create patterns or logos on surfaces. You'll spot them in theaters for scenic effects, at concerts to splash band names across stages, in retail spaces to cast brand marks on floors, and even at weddings for custom monograms on dance floors.
It starts with the artwork file—usually a vector graphic—which gets cleaned up so thin lines don't disappear or thick areas don't overheat. The design is then transferred onto a metal or glass blank using either high-resolution laser etching for steel or precise photo-chemical milling for brass. After that, the gobo is inspected under a magnifier to catch any rough edges before it gets mounted into a projector.
Most gobos are made from stainless steel, brass, or borosilicate glass. Stainless steel holds up to heat well and is budget-friendly for simple shapes. Brass gives finer detail because it can be etched more precisely. Glass gobos are the go-to for full-color or grayscale images since they can handle high temperatures while letting light pass through different density areas.
For metal gobos, a focused laser beam vaporizes tiny portions of the surface to carve out the pattern, leaving clean edges down to about 0.1mm. Glass gobos are trickier: a coating is applied, then the design is photo-etched into that layer, and the unexposed parts get washed away. The result is a high-contrast template that can block or transmit light exactly where needed.
We use a collimated light source and a precision-cut aperture to keep the beam narrow, plus the gobo itself is held in a rigid mount so it doesn't warp from heat. Every unit gets tested with a test projector at various distances, and edge sharpness is measured with a simple grayscale target. If a client sees blur, it's usually because their fixture's focal length doesn't match our gobo size, so we sometimes cut a custom spacer.
LEDs run much cooler, so you can use thinner metal or even polymer gobos without melting them, which means finer detail and faster production. Incandescent or arc-source fixtures push heat past 300°F, so the gobo needs to be thicker stainless or special heat-resistant glass. The opening patterns also differ—LED fixtures often have a smaller gate, so the design might need to be scaled down or re-proportioned.
Standard metal gobos can be cut and shipped within 2–3 business days if the artwork is ready and no revisions are needed. Glass gobos with grayscale or color take about 5–7 days because of coating and baking steps. Rush orders can be done in 24 hours for metal only, but that usually means skipping some of the finer finishing touches.
Yes, and it mostly comes down to physics. On metal, you can't reliably etch features smaller than about 0.15mm or they'll simply burn away. On glass, extremely thin lines below 0.1mm can create a halo effect because light diffracts around edges. Also, if a design has huge solid black areas, heat builds up and can warp the gobo, so we often add tiny cross-bridges or break the design into multiple layers.
Conclusion
The process begins not with machinery but with a client's idea—a logo, a texture, a motif. That digital file becomes the blueprint for something meant to withstand intense heat and light. Standard gobos rarely satisfy because they are mass-produced, limited in detail, and often fail when paired with modern LED or arc lamps. A dedicated factory treats each design as a unique challenge: selecting the right metal thickness, deciding between stainless steel or brass, and using laser cutting or chemical etching to preserve fine lines that off-the-shelf products blur away. On the factory floor, the atmosphere is surprisingly quiet; operators work with micron-level tolerances, inspecting each disc under magnification before it moves on. This is where the craft lives—not in speed, but in the patience to keep every hairline sharp.
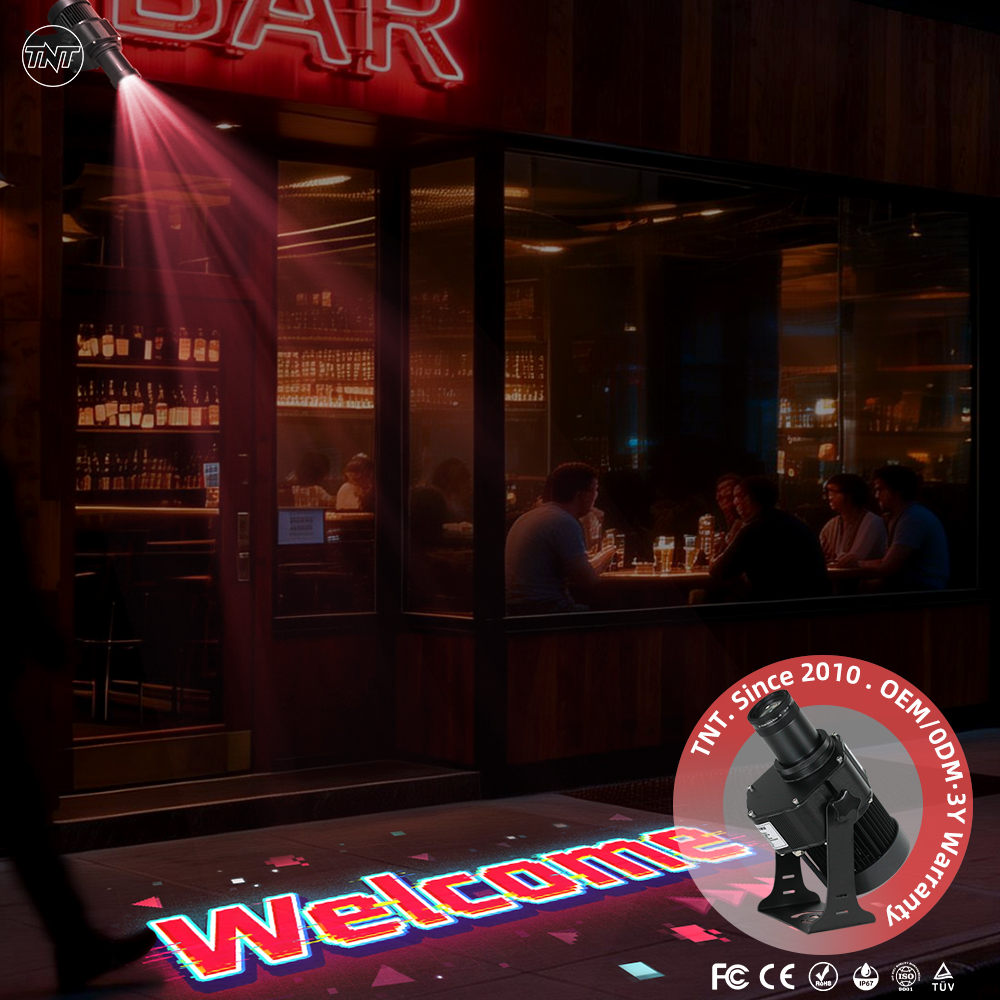
From that point, a digital file transforms into a physical beam. The cut gobo is coated to resist heat, sometimes blackened to improve contrast, then mounted in a holder that aligns it perfectly within the projector's optical path. When the pattern finally meets its lamp, the real test begins: does the projected image hold its shape, or does it warp and bloom under heat? Custom production accounts for lamp type, focal length, and gobo size, ensuring the beam carries the intended pattern cleanly across a stage, wall, or storefront. It is a quiet, exacting trade—one that connects a designer's vision to the physics of light, one cut at a time.
Contact Us
Contact Person: TNT SALE
Email: [email protected]
Tel/WhatsApp: 8613544277910
Website: https://www.tntprojector.com/