Abrasive Jumbo Roll Supplier: How to Choose the Right Partner for Your Business
2026-09-23
Most buying checklists for abrasive jumbo rolls miss what really drives long-term cost: supplier responsiveness, roll consistency, and the ability to customize widths without delay. Before you sign another contract, consider what a partner like SHENZHEN SUN ABRASIVES brings to the table—and what you might be leaving on the floor.
Grind It Before You Buy It: Sample Testing Beats Sales Talk
Most vendors will hand you a polished pitch deck and a list of promises. But a sample run tells you what a sales call never will: how the material actually behaves when it hits your grinder, your tooling, and your tolerance limits. You are not buying a data sheet. You are buying what happens at the spindle.
Grinding a test piece exposes chatter, burn marks, wheel loading, and finish inconsistencies that no amount of talk can hide. It also shows whether the supplier's recommended speeds and feeds match reality or just their marketing assumptions. One hour at the wheel is worth a dozen webinars.
Before you sign the order, ask for a sample that matches your worst-case geometry, not their easiest demo part. Run it on your machine, with your operator, under your deadlines. If it survives that, you have a reason to buy. If it does not, you just saved yourself a very expensive conversation.
Capacity Without Cracks: Can They Deliver When Your Line Runs Hot?
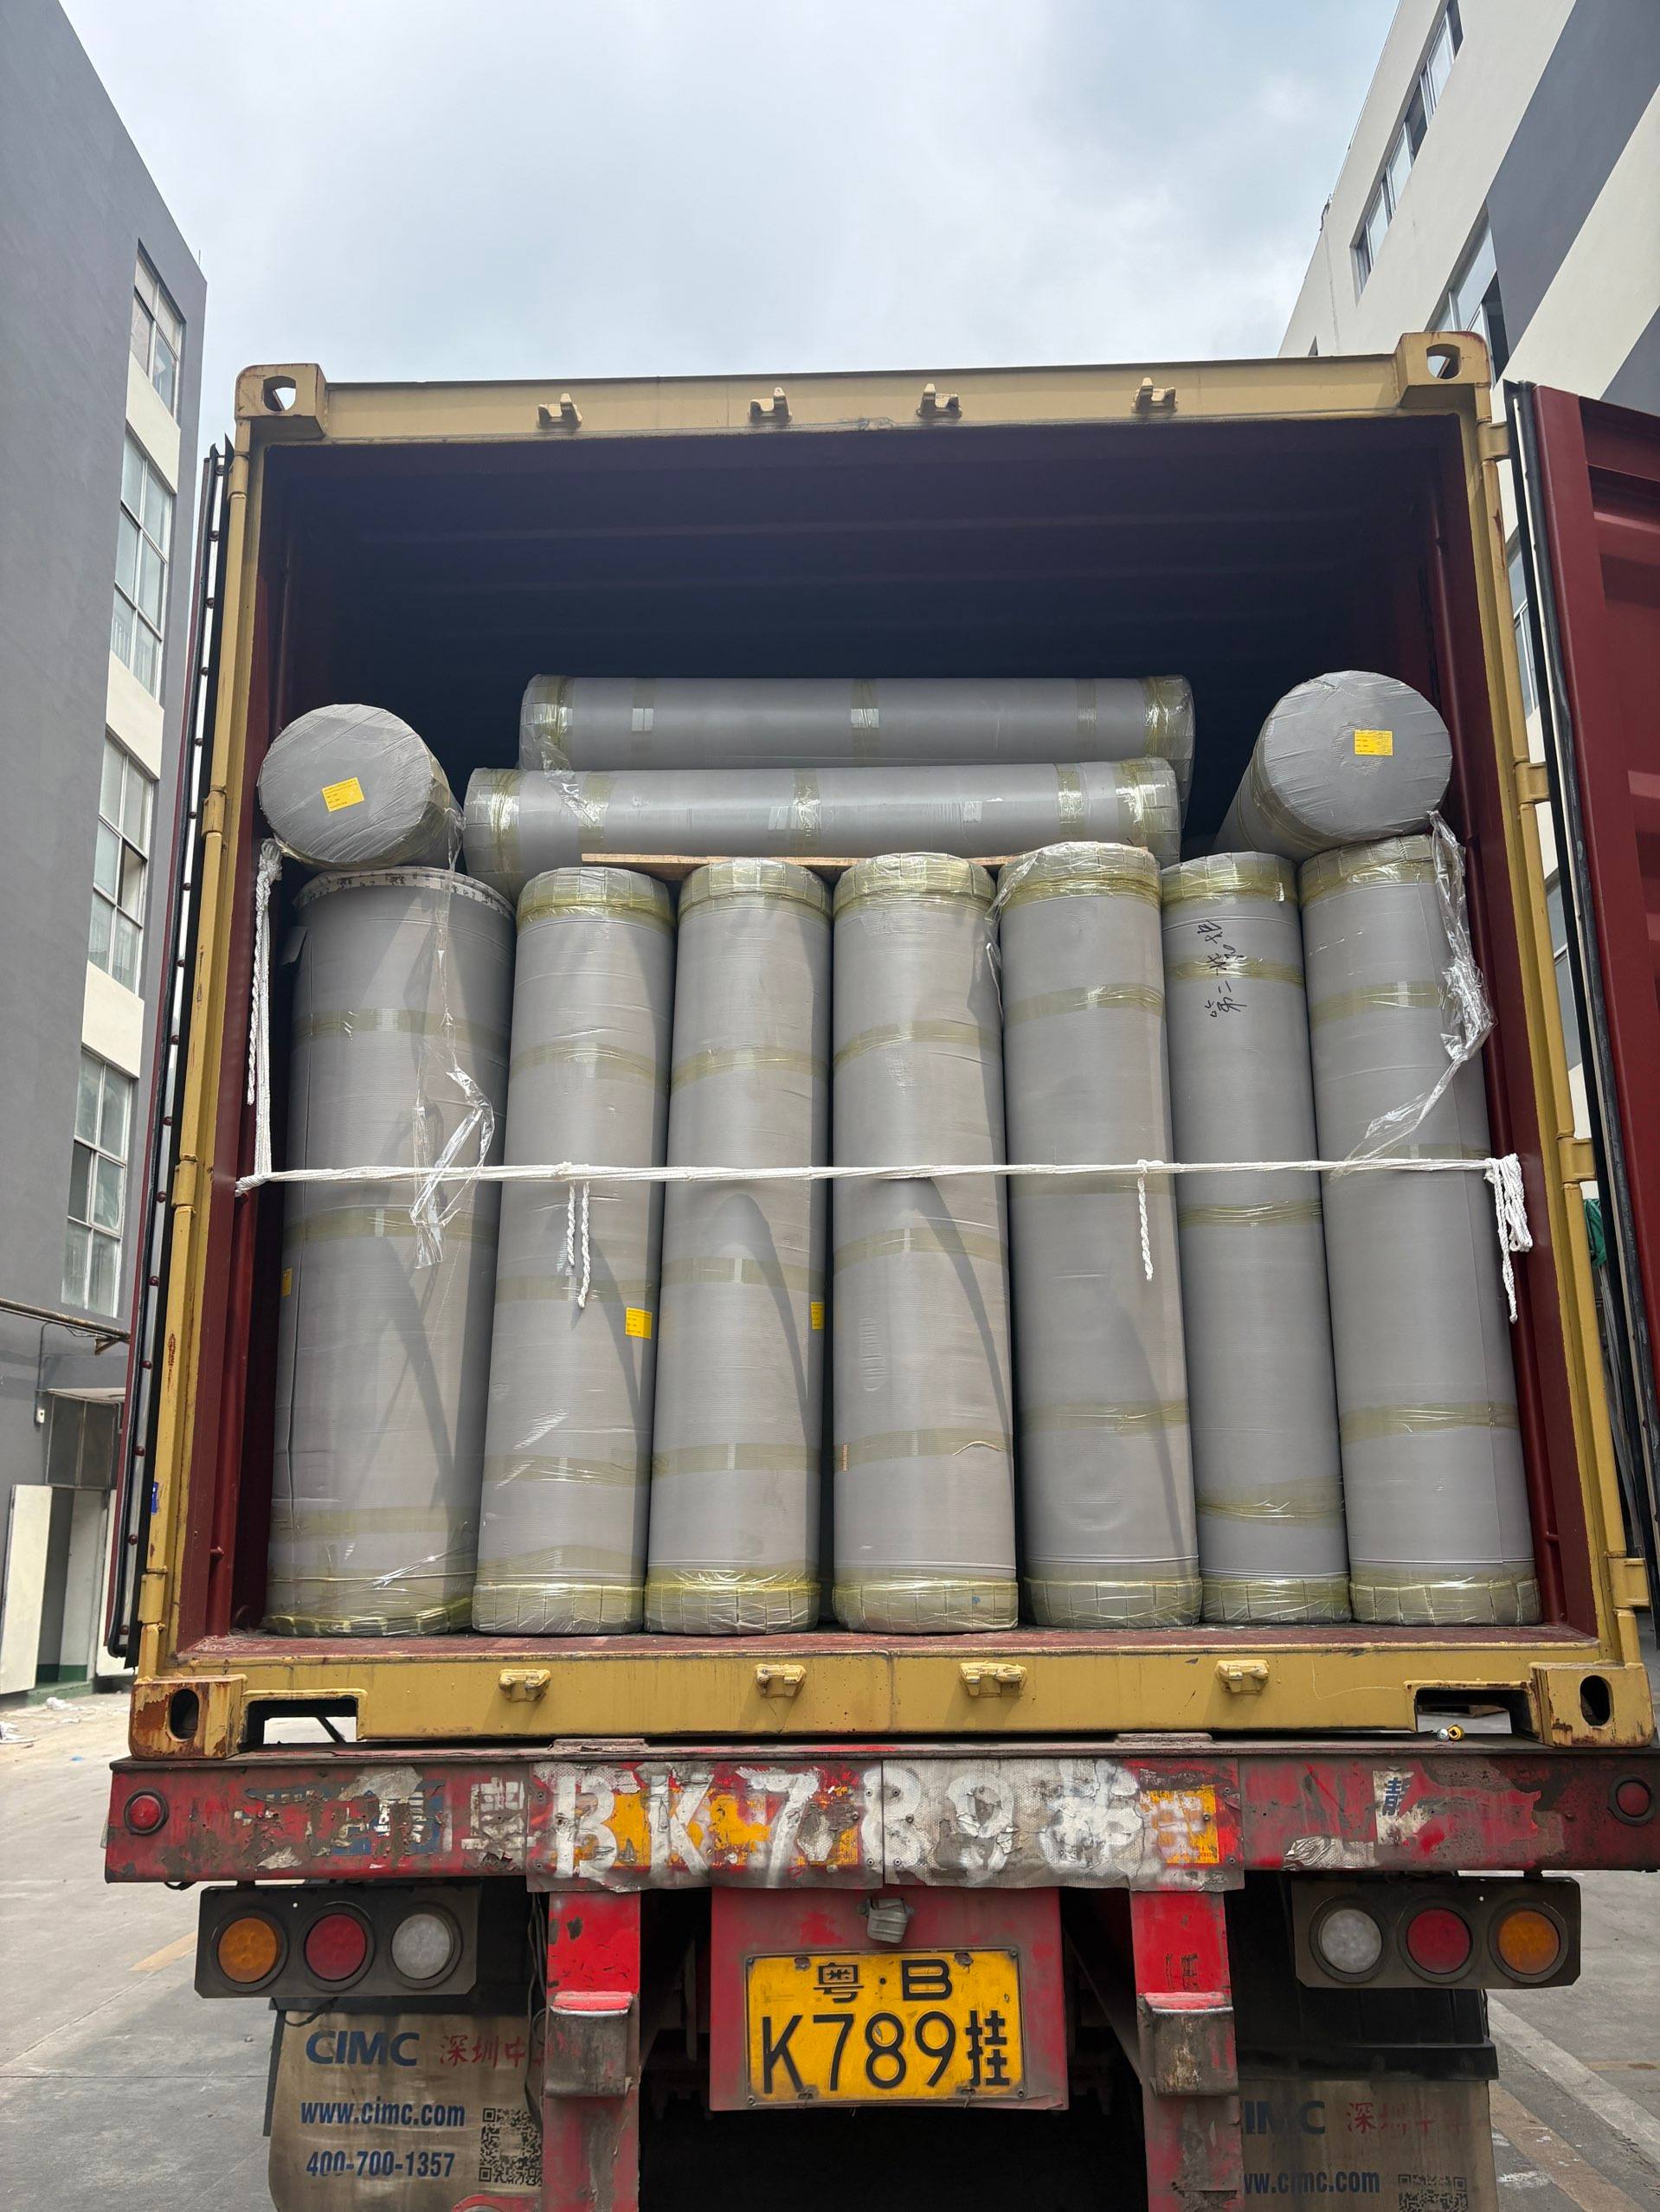
A supplier's brochure may list impressive maximum output, but real capacity shows itself only when orders spike and every shift runs at full tilt. The question isn't whether they can produce a batch; it's whether they can hold tolerances, keep lead times honest, and avoid shipping rushed work when the line is running hot.
Look for the less obvious signals: how they schedule preventive maintenance during peak weeks, whether they cross-train operators so a single absence doesn't stall a cell, and what their scrap rate does when throughput climbs. Facilities that truly understand capacity have already mapped their constraint points and can tell you which machine or process will hit its ceiling first — and what they plan to do about it.
Ask them to walk you through their last true surge. If they can name a specific week when volume jumped by thirty percent and still hit delivery dates without a quality dip, that's worth more than any capacity chart. If they hesitate, keep looking.
Specs Are Nice, But Ask for Results from a Shop Like Yours
Anyone can list horsepower, torque figures, or precision tolerances on a website. But those numbers don't tell you how a machine behaves when it's been running for 14 hours straight, covered in dust, and pushed beyond its original duty cycle. That's where real-world results separate a shop that simply builds things from one that understands your operating conditions.
Instead of comparing spreadsheets, ask for case studies, performance logs, or repair histories from customers who run equipment in environments similar to yours. Look for documented uptime percentages, maintenance intervals that stretch longer than expected, and problem-solving examples where a shop modified a design mid-project because the initial specs didn't hold up. A good fabricator or machinist will be proud to show you those records—not just a glossy brochure.
When you're evaluating a partner, try this: describe your toughest failure from the past year and ask how they would have prevented it. Their answer will reveal more than any tolerance chart. You'll quickly see whether they rely on generic solutions or actually engineer for the ugly, unpredictable side of your work.
The Half-Inch Difference: Why Slitting Tolerances Decide Your Scrap Rate
On a single coil, a half-inch width error looks like a rounding mistake. But slitting tolerances compound fast: a line that runs 2,000 coils a year at an average 0.50-inch oversize is generating 1,000 inches of extra material per coil width. That extra half-inch often becomes the scrap skeleton before the blank ever reaches a die.
Loose slitting tolerances force downstream operations to build in extra trim allowance. If a stamper needs a 12.00-inch blank but the slit strip can arrive at 12.30 to 12.70 inches, the die must be designed to swallow that variance. The result is predictable: every blank carries a wider edge allowance, and that allowance is sheared off and thrown away as scrap. Tightening the slitter from ±0.060 inch to ±0.015 inch removes most of that hidden waste without slowing the line.
One service center tracked the change after retrofitting their slitter with automatic edge position feedback. The half-inch drift had been feeding roughly 2.1 tons of usable steel per shift into the scrap bin. After bringing width variation under 0.040 inch total, the same coils produced nine additional stamped blanks per ton. The difference did not come from buying better steel; it came from not slitting it away.
After the Invoice: Who Fixes a Bad Lot Without Making You Beg?
Once payment clears, the power balance shifts. A defective lot that would have been replaced without question before the invoice now becomes a test of your patience. Suppliers who were responsive during the sale suddenly need “more details” or “internal review.” You end up sending follow-up emails that feel like begging, while the bad product sits in your warehouse.
The fix starts before the invoice is ever issued. Write quality terms that spell out what happens when a lot fails inspection—return shipping, replacement timelines, and penalties for non-compliance. Keep your own test results and photos from the moment goods arrive. This evidence changes the conversation from a favor to a contractual obligation.
If a supplier still stalls, don't chase politely. Send a formal notice with a deadline, referencing the exact clause they breached. Escalate to their management or use a third-party inspection report. You shouldn't have to beg for what you already paid for; the contract should do the demanding for you.
Cheap Rolls, Expensive Downtime: Calculate Your True Cost per Part
When a roll fails mid-run, the invoice price is only the first domino. The real sting comes from the minutes—or hours—your line sits idle while operators scramble for a replacement. A roll that costs 20% less upfront but lasts half as long quietly erodes margin with every unplanned stop. To see the actual cost per part, add the purchase price, installation labor, and lost production value, then divide by the number of good parts that roll produced before it was pulled.
Think of it as cost per thousand impressions, not cost per roll. A $500 roll that runs 200,000 linear feet looks cheaper than an $800 roll that runs 450,000, until you factor in the two extra changeovers, the scrap from machine ramp-up, and the overtime needed to claw back lost throughput. Those hidden line items can easily triple the effective cost of a “bargain” roll.
The calculation isn’t complicated: track roll life, downtime minutes per change, and your line’s profit per minute. Then compare candidates on cost per good part, not sticker price. You might find that paying more for a roll with a harder surface or better core stability actually drops your true cost by 15% or more—simply by keeping the machine running instead of waiting on a wrench.
FAQ
Focus on their track record with roll width consistency and grain adhesion. Ask for sample rolls and run them on your own converting line before committing to anything bigger.
A lot, especially if you convert into discs, sheets, or specialty shapes. The supplier should be able to adjust backing weight, grain type, and splice design without treating every change like a special favor.
Ask how they handle raw material shortages, what their typical lead time is during peak season, and whether they carry buffer stock for repeat customers. Their answers will tell you more than a polished brochure.
Price matters only after performance is proven. A cheaper roll that causes downtime or inconsistent finishes on your converted products will cost far more in rework and customer complaints than you saved upfront.
Give them a real converting issue you have faced, like edge tearing or loading problems, and see if they offer specific, actionable advice rather than generic troubleshooting steps.
It is wise for large or critical runs. Ask for batch-level test data covering grit size distribution, bond strength, and tensile strength, and compare it against your own incoming inspection results.
It affects freight cost and lead time, but nearby is not automatically better. A supplier farther away with stronger consistency and better support may still deliver lower total cost over a year.
Look for a willingness to improve together. A good partner will proactively suggest roll constructions that reduce your waste or increase your line speed, not just repeat the same quote every month.
Conclusion
Choosing the right abrasive jumbo roll supplier starts with ignoring polished sales pitches and demanding proof. Request sample rolls and run them on your own equipment under normal production speeds and pressures. A supplier that hesitates to provide test material or only offers lab data is already telling you something. Beyond the sample, dig into their actual capacity during peak seasons. If your line runs hot and you need a fast turnaround, can they keep up without sacrificing consistency? Ask for references from shops similar to yours, not just big names. A supplier that has solved problems for a business like yours will understand your surface finish requirements and tolerance limits. Pay particular attention to slitting tolerances. A half-inch error may sound minor, but across thousands of parts it drives up scrap, jams, and rework costs, quietly eating your margin.
The relationship does not end when the invoice is paid. Before committing, find out how the supplier handles a bad lot. Will they replace it quickly or make you beg for weeks while your production stalls? A responsive partner treats a defect as an urgent problem, not a negotiation. Finally, stop comparing price per roll in isolation. Cheap abrasive can cause slower cutting, more heat, and more frequent roll changes. Calculate your true cost per finished part, including labor, downtime, and machine wear. A slightly higher upfront price often delivers lower overall cost when the abrasive performs consistently and the supplier stands behind their product. The right partner is not just a vendor; they are an extension of your process control.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn